Godavari Coconuts West Godavari · India
Contact Contact Us

West Godavari Plant Engineering · ₹35+ Cr Integrated Campus

Centrifuge, Heat Pump & Retort Processing Technology

Engineered for clean-label consistency at industrial scale: high-speed disc-stack centrifuges, closed-loop heat pump dehydration chambers, PLC-controlled overpressure retort machines, and closed SS-316 food-grade piping across our 100,000 coconuts/day facility.

Request Plant Technical Brief → Explore 24-SKU Catalogue

Core Processing Systems

Precision Food Engineering Across Wet, Dry & Preserved Lines

01 · Centrifugal Separation Bowl Speed & < 0.1% Moisture Control

High-Speed Centrifuge Technology

Multi-Phase Centrifugal Clarification for Virgin Coconut Oil & Milk Emulsions

Continuous high-G stainless-steel disc-stack centrifuges separate freshly pressed coconut milk emulsion rapidly into crystal-clear Virgin Coconut Oil, high-fat cream, and aqueous fractions inside closed SS-316 vessels—eliminating chemical solvents, bleaching earths, and harsh deodorization.

  • Rapid continuous 3-phase centrifugal oil-cream-water separation
  • Retains natural lauric acid fraction, fresh coconut aroma & optical clarity
  • Closed stainless-steel bowl architecture prevents ambient oxidation
  • Achieves < 0.1% residual moisture with zero chemical refining

Target Lines: Virgin Coconut Oil · Coconut Cream · Coconut Milk

02 · Clean Drying Engineering 45–65°C Closed-Loop Airflow & < 3% RH Targets

Closed-Loop Heat Pump Dehydration

Energy-Recovering Clean Air Dehumidification for Fruits, Vegetables & Desiccated Kernel

Instead of open combustion or soot-prone fuel dryers, our closed-loop heat pump chambers continuously dehumidify and recirculate filtered dry air across food-grade stainless trays. Controlled gentle temperatures (45–65°C) extract moisture evenly without scorching sugars or dulling natural pigments.

  • 100% closed-loop clean drying—zero smoke, soot, or flue-gas contact
  • Low-temperature moisture extraction preserves vibrant fruit colour & aroma
  • Built-in heat recovery lowers specific thermal energy per kg dried
  • Consistent target moisture (< 3.0% desiccated kernel; < 5–8% produce)

Target Lines: Desiccated Coconut Powder · Coconut Chips · 7 Dehydrated Fruits & Vegetables

03 · Thermal Preservation PLC F0 Lethality & Overpressure Ramp Verification

State-of-the-Art Retort Machines

PLC-Controlled Steam & Overpressure Retort Autoclaves for Ambient Pack Integrity

Automated steam and water-spray overpressure retort machines apply calibrated heat-penetration curves, F0 lethality tracking, and pressure-balanced cooling to sealed cans, glass bottles, and retortable jars—delivering commercial sterility and long ambient storage readiness without chemical preservatives.

  • PLC-logged F0 lethality, temperature probes & overpressure profiles per batch
  • Balanced air overpressure during heating/cooling prevents cap distortion or glass shock
  • Zero synthetic preservatives needed for multi-month ambient distribution
  • Lot-coded digital sterilization records attached to batch QA release

Target Lines: Coconut Milk & Cream · RTD Coconut Milk Beverages · Nata de Coco · Pickled Jars

04 · Prep, Filtration & Lab QA 5-Gate In-House Analytical Release & Lot Traceability

SS-316 Piping, Metal Detection & 5-Gate Lab

Farm-Gate Grading to Pre-Shipment COA Traceability Under One Roof

Supporting every centrifuge, heat pump dryer, and retort autoclave are food-grade stainless-steel kernel preparation lines, multi-micron polish filtration, automated bottle/jar capping torque checks, inline metal detectors, CIP (Clean-in-Place) loops, and our in-house analytical testing lab.

  • Clean-in-Place (CIP) closed wash circuits across wet oil and milk lines
  • Multi-micron polish filtration and inline ferrous/non-ferrous metal screening
  • In-house peroxide value, FFA, moisture, Brix, acidity & seal vacuum testing
  • Batch-coded farm-to-carton traceability supporting domestic & export COA packets

Target Lines: All 21 Coconut, Dehydrated & Pickled SKUs · OEM Private Label Runs
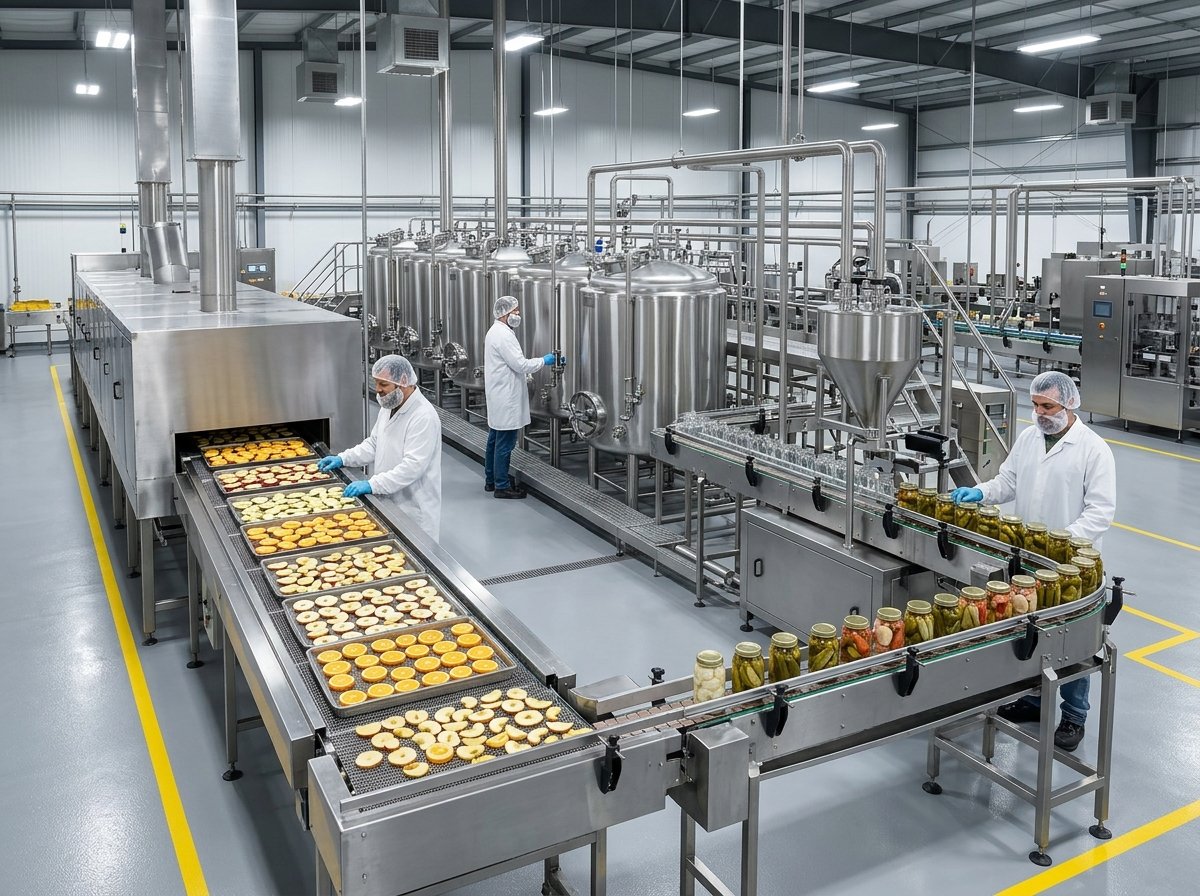
Step-by-Step Line Workflows

Fruit & Vegetable Dehydration · Brine & Vinegar Pickling

Stainless steel industrial fruit and vegetable dehydration tunnel, stainless brining vats, and automated conveyor jar-filling line

Moisture-Controlled Ingredient Processing

Dedicated Dehydration Infrastructure

Beyond coconut processing, Godavari Coconuts operates dedicated closed-loop heat pump dehydration lines to convert fresh seasonal produce into low-moisture ingredients tailored to domestic and international buyer specifications.

Processing Workflow

  1. 01.Fresh fruit & vegetable selection
  2. 02.Potable water washing and grading
  3. 03.Precision cutting and pre-treatment
  4. 04.Moisture-controlled closed-loop dehydration
  5. 05.Quality inspection & barrier packaging

Product Categories & Uses

  • · Dehydrated Fruits (Mango, Pineapple, Banana, Papaya, Jackfruit)
  • · Dehydrated Vegetables (Carrot & Tomato)
  • · Fruit Ingredient Cuts & Custom Dice
  • · Vegetable Ingredient Flakes & Powders
  • · Customized Dehydrated OEM Products

Applications: Food Manufacturing · Healthy Snacks · Bakery & Cereals · Ready-to-Cook Foods · Bulk Ingredient Supply

Line-by-Line Specifications

Machinery Allocation & Quality Control Matrix

Technology System Assigned Product Lines Engineering Advantage Control Parameter
High-Speed Disc-Stack Centrifuge Virgin Coconut Oil, Coconut Milk, Coconut Cream Non-chemical phase separation preserving fresh kernel aroma and optical clarity Moisture < 0.1% · FFA controlled
Closed-Loop Heat Pump Dehydrators Desiccated Coconut, Coconut Chips, 7 Dehydrated Fruits & Vegetables Zero flue-gas clean air dehumidification preserving natural pigments and nutrients 45–65°C curve · Uniform moisture lock
PLC Overpressure Retort Autoclaves Coconut Milk, Beverages, Nata de Coco, Pickled Jars Precision thermal sterilization and balanced cooling with zero chemical preservatives Automated F0 logging · Seal integrity verified
CIP Sanitation, Filtration & Metal Screening All Retail, HoReCa & Bulk Industrial Formats Closed SS-316 transfer, polish filtration, torque capping & 5-gate lab COA 100% batch-coded lot release

Food Safety, Quality & Export Compliance

Certifications, Lab Testing & Export Accreditations

Clear separation between active daily plant licensing/lab QA protocols and international export & organic certifications progressing through commissioning.

Active Plant Food Safety & Lab Protocols

ACTIVE PROTOCOL · PLANT LICENSING

FSSAI Food Safety Licensing

Foundational Indian food safety hygiene, potable water checks, and batch traceability.

ACTIVE PROTOCOL · IN-HOUSE LAB

5-Gate Lab QA & Batch COA

Every lot verified for residual moisture, peroxide stability, pH/acidity, and closure seals.

ACTIVE PROTOCOL · EXPORT DESK

Import-Export Code (IEC)

Registered Indian export entity supporting direct FOB Visakhapatnam, Kakinada & Krishnapatnam dispatches.

In Audit & Export Commissioning Roadmap

ISO 22000 / HACCP & BRCGS

IN AUDIT · EXPORT COMMISSIONING

Structured GFSI hazard analysis critical control point documentation across processing lines.

APEDA Export Registration

IN COMMISSIONING · EXPORT DESK

Agricultural & processed food export compliance for international container shipments.

USDA / NPOP Organic Readiness

GROVE AUDIT · SEGREGATED LOTS

Traceable West Godavari grower clusters aligned for certified organic segregation.

U.S. FDA & Kosher / Halal

IN PROGRESS · IMPORTER MARKETS

Facility registration & buyer-requested Kosher/Halal batch certifications for US/MENA.

FSSAI Food Safety Licensing

ACTIVE

5-Gate Lab QA & COA

ACTIVE

APEDA · ISO 22000 / HACCP

IN AUDIT

BRCGS & Kosher / Halal

IN AUDIT

USDA / NPOP Organic

IN AUDIT

U.S. FDA & MSME ZED

IN AUDIT

Godavari Coconuts

Essential Security & Session Cookies

Required for CSRF form security, session reliability, and storing your consent choice.

Always Active
View Full Cookie Declaration →